I. Why Gate Valves Require Dedicated Lock‑Out Devices
Within
the industrial LOTO (Lockout‑Tagout) system, gate valves are one of the
most common energy‑isolation points. Piping may carry steam,
high‑pressure water, chemicals or flammable gas. Unless a valve is
securely fixed in the closed position, maintenance personnel working
downstream are constantly exposed to the risk of accidental valve
reopening.
However,
gate valves rank among the most difficult isolation points to secure.
Unlike circuit breakers with standard locking holes or push‑buttons with
recesses, gate valves are fitted only with a round handwheel that can
be rotated to open the valve with minimal effort. A simple warning tag
provides no physical restraint at all. A physical device must be used to
lock the handwheel in place so that reliable energy isolation can be
achieved.
A
valve lockout device is designed for exactly this purpose. It encases
or clamps onto the valve handwheel to prevent rotation, and is secured
with a safety padlock. This converts a “closed valve” into a “valve that
cannot be opened”.
II. Step One for Selection: Identify Your Valve Properly
Incorrect
device selection is the leading cause of failed gate‑valve lockout.
Three key parameters must be confirmed before purchasing:
-
Handwheel Diameter This is the core parameter for selecting a gate‑valve lockout. Lockout
devices are graded according to handwheel diameter, with standard ranges
covering 1 inch up to 13 inches and above. Adjustable‑range units are
required for sizes beyond standard coverage. Match the measured
handwheel diameter against the device’s specification range. It is
better to allow slight clearance than to force‑fit: excessive tightness
prevents installation, while excessive looseness results in insecure
clamping.
-
Handwheel Type The two most common variants are spoked handwheels (with open gaps
between spokes) and solid‑disc handwheels (solid or nearly‑solid
circular face). Lockout devices for spoked handwheels clamp into the
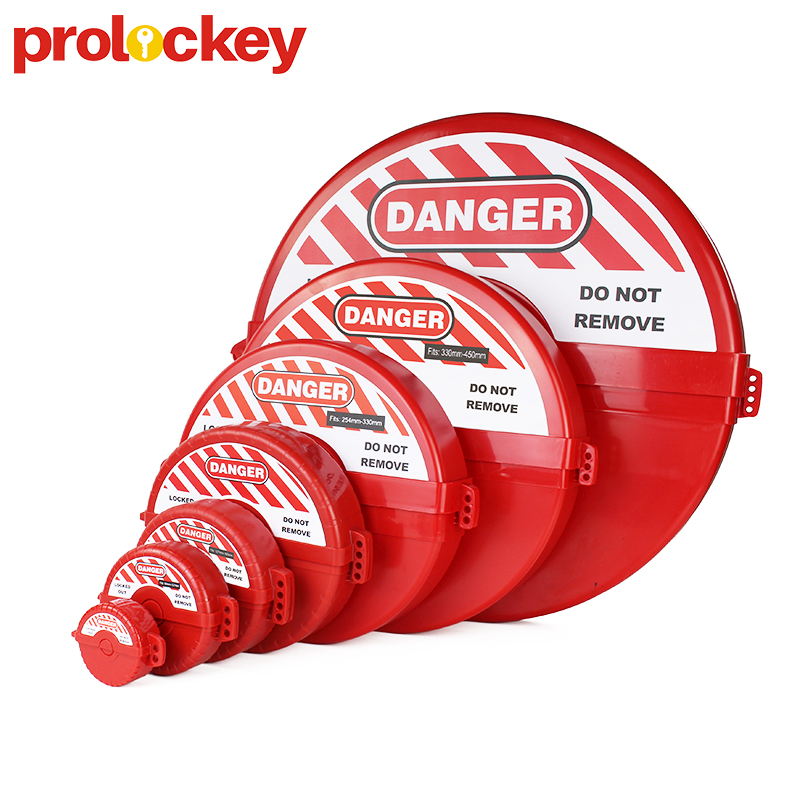
gaps between spokes. Solid‑disc handwheels require two‑piece
enclosure‑style locks that close around the full circumference. These
two designs are structurally incompatible; buying the wrong unit will
render it unusable.
-
Valve Category Strictly speaking, gate‑valve lockout devices are intended exclusively
for gate valves. On‑site cross‑use with ball valves, butterfly valves
and globe valves frequently occurs, yet each of these requires a
distinct lockout mechanism. Ball‑valve locks restrain lever rotation,
while butterfly‑valve locks secure the operating handle. If your pipe
rack contains mixed valve types, purchase dedicated locks for each
category rather than relying on a single universal‑fit solution.
III. Step Two for Selection: Choose the Right Structure
Three main structural designs are available for gate‑valve lockout devices, each suited to different scenarios:
-
One‑Piece Universal Gate‑Valve Lock The most common entry‑level solution. Fabricated as an
injection‑moulded engineering‑plastic housing with movable internal jaws
to grip handwheel spokes or edges. It covers a relatively wide diameter
range (for example 1 – 6.5 inches) and offers high versatility, making
it ideal for older facilities with a large variety of existing valve
sizes. The drawback is that the clamping jaws may fail to grip highly
irregular‑shaped handwheels.
-
Two‑Piece Enclosure‑Style Gate‑Valve Lock Consists of upper and lower shells that fully enclose the handwheel,
fastened together with screws before padlocking. This design tolerates
nearly all handwheel profiles and works equally well for spoked and
solid‑disc types, delivering high locking strength. It is the mainstream
option for high‑safety‑risk sites such as chemical plants and power
stations. The downside is that separate units must be purchased for
distinct diameter bands, with each device covering only a narrow size
range.
-
Adjustable‑Range (Multi‑Fit) Gate‑Valve Lock Equipped with sliding jaws or extendable arms to accommodate a broad
spectrum of handwheel diameters, typically from 2 inches to 13 inches.
Perfect for contractors and maintenance crews working at multiple sites
with unknown valve specifications, as a small set can cover most
encountered valves. Its disadvantages include a more complex build and
longer on‑site adjustment time for every application.
IV. Step Three for Selection: Material and Colour Considerations
Material:
Most commercial gate‑valve locks are manufactured from engineering
plastics such as modified ABS or nylon. Plastic‑based lockouts are
non‑conductive, rust‑proof, resistant to most chemical agents and
lightweight — well suited to long‑term exposure in industrial piping
environments. For steam valves operating at elevated temperatures,
verify the device’s temperature rating (standard engineering plastics
generally sustain continuous exposure between 80 °C and 100 °C);
metal‑constructed lockouts should be selected above this threshold. For
environments with strong acids or alkalis, cross‑check material
chemical‑resistance data.
Colour:
Gate‑valve locks are available in multiple standard colours including
red, yellow, blue, green and orange. Align your colour choices with your
facility’s internal LOTO colour‑coding scheme. For instance, red
commonly signals “Isolated — Do Not Operate”, and yellow may indicate
“Contractor‑Applied Lockout”. Distinct colours enable staff to identify
isolation status visually from a distance along pipe corridors.

 Address: Tangxia Industrial Park, North Baixiang Town, Yueqing, Zhejiang, China
 Name: Miya
 Tel: 0086-577-62968730
 Fax: 0086-577-62531320
 E-mail:
 Skype:
 QQ: